process guide
Stud Welding Explained: Process, Equipment & Applications
Understanding arc and capacitor discharge stud welding, the equipment involved, and where the process is used.
Stud welding uses a specialised gun to join a metal stud directly to a workpiece with heat and pressure from an electric arc or a capacitor discharge; no drilling or pre-existing holes are required. The two main processes, arc and CD (capacitor discharge) stud welding, suit different stud sizes and material thicknesses. This guide explains how each process works, the equipment involved, and the industries that rely on stud welding.
If you're ready to buy, browse our stud welders for sale. Otherwise, read on for how the process works.
Because a stud welder only needs access to one side of the workpiece, it's often the fastest way to attach a fixing where drilling through or reaching the reverse side isn't practical. That single-sided access, combined with a weld that's typically as strong as the base metal, is why stud welding has become a standard process across automotive repair, structural construction, and general fabrication. Not just a niche technique for specialist applications.
What Is Stud Welding?
Stud welding joins a metal stud, pin, or similar fastener to a metal workpiece by melting both surfaces at the point of contact and fusing them under pressure. A stud welding gun holds the stud in position, an electric arc or capacitor discharge generates the heat, and a spring or plunger mechanism drives the stud into the molten pool to complete the bond. No drilled hole, nut, or bolt is needed; the stud becomes a permanent, welded fixing.
How Does Stud Welding Work?
The stud welder gun positions the stud against the workpiece and triggers an electrical charge. This creates an arc between the tip of the stud and the base metal, which melts a small area on both surfaces. A ceramic ferrule (in arc welding) or the gun's own tip pressure (in CD welding) contains the molten metal and shields it from the surrounding air while the stud is plunged into the weld pool. The metal solidifies in seconds, fusing the stud to the workpiece with a weld that runs through the full contact area rather than sitting on the surface.
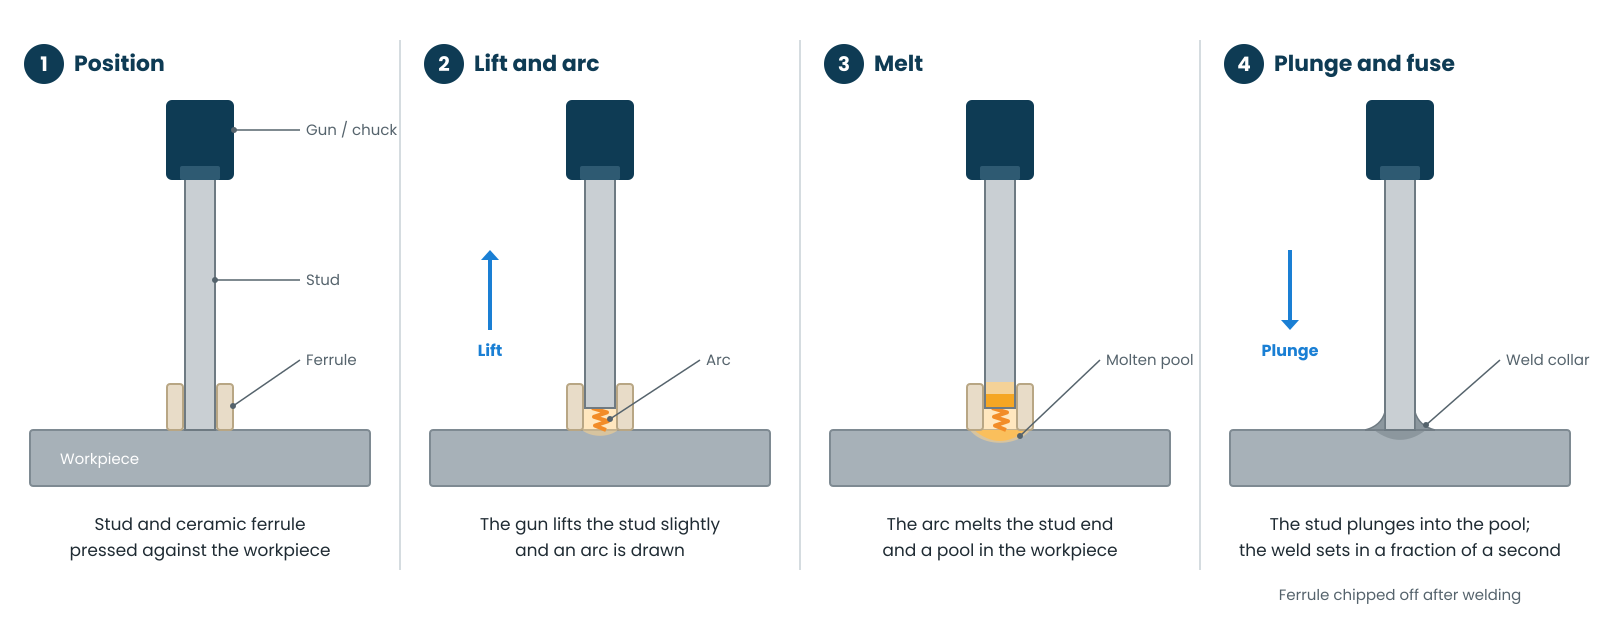
What's the Difference Between Drawn Arc, Short Cycle and CD Stud Welding?
There are three main stud welding processes. They differ in how long the weld takes, how much heat goes into the workpiece, and the stud sizes they can handle.
- Drawn arc stud welding (often just called arc stud welding) lifts the stud slightly off the workpiece to draw an arc, melts the end of the stud and a small area of the base metal, then plunges the stud into the molten pool. A ceramic ferrule around the stud shields the weld and shapes the collar. The longer weld cycle gives deep penetration for large studs and thick plate, which makes it the standard process for structural work and shear studs.
- Short cycle stud welding is a faster version of drawn arc. It uses a higher current for a much shorter time, usually without a ferrule. That limits heat input and marking on the reverse side, so it suits small to medium studs on thinner sheet, and it's widely used in automotive and sheet metal production.
- Capacitor discharge (CD) stud welding releases energy stored in capacitors in a single burst of a few milliseconds. A small tip on the end of the stud starts the arc. Because the heat is so brief, CD can fix small studs to very thin sheet with little or no marking on the visible face.
|
|
Drawn arc |
Short cycle |
CD |
|---|---|---|---|
|
Weld time |
About 0.1–1.5 seconds |
About 10–100 milliseconds |
About 1–3 milliseconds |
|
Typical stud size |
Medium to large, including shear studs |
Small to medium, up to around M10 |
Small, around M3–M8 |
|
Base material |
Medium to heavy plate |
Thin to medium sheet |
Very thin sheet upwards |
|
Ferrule |
Yes (ceramic) |
Usually not |
No |
|
Reverse-side marking |
Likely on thinner material |
Limited |
Minimal |
|
Typical power supply |
Three phase |
Single or three phase, depending on size |
Single phase |
|
Best for |
Structural steel, shear studs, heavy fabrication |
Automotive, enclosures, production lines |
Thin sheet, panels, cabinets, visible faces |
Which process to use depends on the stud size, the material thickness and whether the reverse face has to stay unmarked. The processes aren't generally interchangeable for a given job, so start from the stud and the material, then choose the machine.
What Types of Studs Are Used in Stud Welding?
Stud welding covers several stud designs, chosen for the application and the fixing they need to create:
- Threaded studs: externally threaded fasteners welded in place so components, brackets or fittings can be bolted on afterwards. Common in panel and enclosure assembly.
- Shear connectors (shear studs): headed studs welded to structural steel beams, then bonded using a poured concrete slab. This transfers shear force between the steel and concrete, allowing the two to act as one composite structural section. Used extensively in bridge decks and composite floor construction.
- Headed studs and pins: plain fasteners without threads, used where the stud itself is the fixing point, such as insulation pins or standoffs.
Choosing the right stud type and diameter for the base material and load is as important to weld quality as the welding process itself.
Shear Studs and Through-Deck Welding
Shear connectors, usually called shear studs, are headed studs welded to the top flange of steel beams. When the concrete floor slab or bridge deck is poured around them, they lock the steel and concrete together so the two work as one composite section. That lets designers use lighter beams and shallower floors than steel or concrete could manage alone.
The most common shear stud is 19 mm in diameter, with 16 mm and 22 mm also widely used. The length is set by the depth of the slab.
Through-deck welding
In composite floors, profiled steel decking is laid over the beams as permanent formwork for the concrete. The studs are then welded through the decking into the beam below, which fixes the deck and creates the shear connection in one operation. For a sound weld, the decking must sit tight to the beam, the top flange must be left unpainted, and the area must be dry. Where those conditions can't be met, the decking is pre-holed or the studs are welded to the beams before the decking goes down.
What shear stud welding needs
Shear studs are welded by drawn arc with ceramic ferrules. They're among the most demanding stud welding jobs: a 19 mm stud needs well over 1,500 amps for close to a second, and welding through decking needs more. That means a large three-phase drawn arc unit, run on site from a suitable mains supply or a large generator. Our Diesel Welder-Generators & Site Power Guide covers sizing site power.
Which Materials Can You Stud Weld?
Stud welding works on most weldable metals, as long as the stud material is matched to the base material and the process suits the thickness.
- Mild steel is the most common combination and works with all three processes, from small CD pins to large shear studs.
- Stainless steel studs weld well to stainless sheet and plate by drawn arc, short cycle or CD, with settings adjusted for the material. Stainless studs are common in food, pharmaceutical and marine work, where corrosion resistance matters.
- Aluminium is most often stud welded by CD, which suits the thin sheet aluminium is usually used in. Drawn arc welding of aluminium is possible, but it needs an inert shielding gas in place of the ceramic ferrule. In either case, the oxide layer on the surface must be removed first.
- Brass and copper studs are available for CD welding, mainly for electrical and earthing connections.
- Galvanised and coated steel can affect weld quality, so the weld area is usually cleaned back to bare metal. The main exception is through-deck shear stud welding, which is designed to weld through galvanised decking.
Threaded studs are the most widely used type across all these materials. They're welded in place so components, brackets or panels can be bolted on afterwards. Internally threaded studs (with a tapped hole rather than an external thread) are also available where a flush fixing is needed.
What Equipment Do You Need for Stud Welding?
A working stud welding setup requires a small number of core pieces of equipment:
Getting consistent results depends on matching every part of this stud welding equipment list to the job. The wrong collet size or an incorrect stud-to-gun match is one of the most common causes of a failed weld.
Need studs, collets or ferrules for a machine you already have? We can source parts for most stud welders, so get in touch.
View our stud welding machines for sale →
What Power Supply Does a Stud Welder Need?
A stud welder's power needs depend mainly on the process and the largest stud it's built to weld.
- CD stud welders charge their capacitors steadily between welds, so they run on a standard single-phase supply. That makes them easy to use in workshops and on site.
- Short cycle and smaller drawn arc units come in single-phase and three-phase versions. Modern inverter machines in this range are lighter and draw less from the supply than older transformer units of the same capacity.
- Large drawn arc and shear stud welders need a three-phase supply. They deliver very high currents for up to a second or more, so the supply has to be rated for the machine's peak input, not just its average use. On site, they're usually run from a large generator.
Before buying or moving a machine to a new site, check its rating plate for the input voltage, phase and current, and make sure the supply and any generator are rated to match.
How to Use a Stud Welder: Step by Step
The routine is much the same whichever process you use. Drawn arc adds a ceramic ferrule and a lift-and-plunge action in the gun; CD skips both. Always work from the machine manufacturer's settings chart and safety guidance, and wear eye protection rated for arc welding.
- Choose the stud and process for the job. Match the stud type and diameter to the load and to the thickness of the base material. Drawn arc suits larger studs on thicker plate, while CD suits small studs on thin sheet. The stud supplier's data will give the minimum material thickness for each stud size.
- Prepare the surface. The stud needs clean, bare metal to weld to, so remove rust, mill scale, paint, oil and heavy primer from the weld area. The exception is through-deck shear stud welding, where the process is designed to weld through galvanised steel decking.
- Fit the earth clamp. Clamp onto clean metal close to the weld area. On larger drawn arc work, two clamps on opposite sides of the workpiece help balance the current and reduce arc blow (where the arc is pulled to one side).
- Load the gun. Fit the collet or chuck that matches the stud diameter and push the stud fully home. For drawn arc, fit a ceramic ferrule over the stud and set the lift and plunge as the gun's manual specifies.
- Set the machine. On a drawn arc machine, set the welding current and weld time for the stud size. On a CD machine, set the charging voltage. Make a few test welds on scrap of the same material and thickness before starting on the job.
- Position the gun square to the work. Hold the gun at 90° to the surface and press down so the stud (and ferrule, for drawn arc) sits firmly against the work. Hold it steady; any tilt shows up as a one-sided weld.
- Trigger the weld. Press the trigger and keep the gun still while the machine runs the weld cycle, which takes a fraction of a second. Then lift the gun straight off the stud without twisting or levering it.
- Remove the ferrule and check the weld. For drawn arc, chip the ceramic ferrule away. A good weld shows an even collar of weld metal all the way round the base of the stud. Bend-test the first studs of each shift or setting change (see Weld Quality and Inspection below).
If you're choosing a machine for a specific job, our team can help you match the process and stud range to your work. Browse our stud welding machines for sale or get in touch.
Weld Quality and Inspection
A stud weld is quick to make, so it's easy to check every one by eye and test a sample properly.
- Visual check: a good weld shows an even collar of weld metal all the way round the base of the stud, and the stud stands square to the surface. On drawn arc welds, the ferrule shapes the collar; on CD welds, look for a small, even flash. Check the welded length too: a stud that's noticeably shorter or longer than expected points to a settings problem.
- Bend test: bend the first studs of each shift, or after any change in settings or material, with a hammer or a length of tube over the stud. The weld shouldn't crack; if anything fails, it should be the stud, not the weld.
- Torque test: threaded studs can be checked by tightening a nut to a set torque.
Common faults and their usual cause
|
Fault |
Usual cause |
What to check |
|---|---|---|
|
Collar on one side only |
Arc blow, or the gun not held square |
Earth clamp position (try two clamps), gun angle |
|
Incomplete collar or poor fusion |
Too little current or weld time, dirty surface |
Settings, surface preparation |
|
Heavy spatter or undercut |
Too much current or weld time |
Settings, stud lift and plunge |
|
Porosity (holes in the weld) |
Oil, paint, moisture or damp ferrules |
Surface cleaning, ferrule storage |
|
Marking or burn-through on the reverse side |
Too much heat for the sheet thickness |
Settings, or switch to CD or short cycle |
|
Stud not fully plunged |
Plunge set too short, gun binding |
Gun setup and condition |
Standards: arc stud welding procedures and testing are covered by BS EN ISO 14555, and the studs and ceramic ferrules themselves by BS EN ISO 13918. Structural shear stud work in the US follows AWS D1.1. For structural projects, the project specification will say which applies.
What is stud welding used for?
Stud welding is used wherever a strong, single-sided fixing is needed without drilling through the material:
- Structural construction. Shear studs welded to steel beams create composite steel and concrete construction, most visibly in bridge decks and multi-storey floor slabs. Nelson stud welding machines are industry favourites here.
- Automotive. Panel repair and bodywork use CD stud welding to attach pull pins and fixings to bodywork without marking the visible face of the panel.
- General fabrication and manufacturing. Threaded studs and pins are welded to sheet metal enclosures, cabinets and brackets as a faster alternative to drilling and tapping.
- HVAC and insulation. Pins are stud welded to ductwork and cladding to hold insulation in place without penetrating the opposite face.
- Shipbuilding and marine. Studs fix insulation, linings, cable trays and fittings to decks and bulkheads, where drilling through would compromise the hull or watertight structure.
- Oil, gas and power generation. Studs and anchors hold insulation and cladding on vessels and pipework, and secure refractory linings inside furnaces and boilers.
- Cladding and façades. CD studs fix panels, signage and architectural metalwork from behind, leaving the visible face clean.
Whatever the application, the right machine comes down to the stud size, the material and the power available on site. Browse our stud welding machines for sale, or talk to our team about a specific job.
FAQ:
What is a stud gun?
A stud gun is the handheld part of a stud welding setup. It holds the stud in a collet sized to its diameter and is connected to the stud welder, which supplies and controls the welding current. Pulling the trigger starts the weld cycle, and the gun plunges the stud into the molten metal to complete the weld in a fraction of a second.
What's the difference between drawn arc and CD stud welding?
Drawn arc stud welding (often just called arc stud welding) uses a longer, continuous arc, suited to larger studs and thicker material. CD (capacitor discharge) stud welding uses a short, high-current burst, suited to thin sheet and small studs.
What is a shear stud used for?
A shear stud is a headed fastener welded to a structural steel beam and embedded in a poured concrete slab, transferring shear force between the steel and concrete.
What are Nelson studs?
Nelson is one of the original and best-known stud welding brands, and "Nelson studs" is often used as shorthand for shear connectors: headed studs welded to steel beams, or through metal decking, and embedded in concrete. The name is also used more loosely for other weld studs. We buy and sell Nelson stud welders.
What equipment do I need for stud welding?
A stud welder machine (power source), a weld stud gun, matching studs, collets sized to the stud diameter, and, for arc welding, ceramic ferrules to shield the weld.
Can stud welding be used on stainless steel and aluminium?
Yes. Stud welding is used on mild steel, stainless steel and aluminium, with the process and settings adjusted for the material and stud combination.
Is a stud weld as strong as the base metal?
Set up correctly, a stud weld fuses through the full contact area rather than sitting on the surface, producing a bond that's typically as strong as the surrounding base metal, provided the stud type, size and process match the application.
